A small colored detail repeated across hundreds of layers can consume more filament in transitions than it leaves in the product. The correct response is not to reduce every flush volume blindly. First separate model material, transition waste, additional machine time, and accepted output; then change the transition sequence, geometry, or batch while validating color quality.
Calculation Model
Separate transition overhead from product material
Question: How much cost does the chosen color-transition plan add to each accepted part?
The model uses slicer-reported categories and user-entered prices. It does not claim a typical purge ratio, color-pair result, or measured AMS performance.
transition overhead per accepted part = ((flush + tower grams) × weighted price/g + added machine hours × hourly rate) ÷ accepted quantityVariables
Replace every example input with the job being quoted
| Symbol | Meaning | Unit | Input source |
|---|---|---|---|
| F | Flush material reported for the plate | g | Slicer category when explicitly available |
| W | Prime-tower material reported for the plate | g | Slicer category when explicitly available |
| ΔT | Multicolor time minus comparable single-color time | h | Difference between two same-geometry slices |
| N | Accepted parts sharing the overhead | parts | Scenario quantity after rejected parts |
Scenario Analysis
Modeled example results
These are arithmetic examples—not measurements, tests, benchmarks, or claims about typical printers. Change the inputs to see which assumption controls the decision.
| Modeled scenario | Inputs changed | Example result | How to read it |
|---|---|---|---|
| Single-part example | F = 42 g; W = 10 g; $0.025/g; ΔT = 1.5 h; $1.20/h; N = 1 | $3.10 transition overhead/part | $1.30 material plus $1.80 machine time is assigned to one part. |
| Four accepted copies | Same 52 g and 1.5 h plate overhead; N = 4 | $0.78 transition overhead/part | Shared overhead falls per part only if all four copies are accepted. |
| Higher-price material | F + W = 52 g; $0.040/g; ΔT = 1.5 h; $1.20/h; N = 1 | $3.88 transition overhead/part | Weighted waste price matters when an expensive color carries transitions. |
| Transition-heavy plate | F = 90 g; W = 15 g; $0.025/g; ΔT = 2.5 h; $1.20/h; N = 1 | $5.63 transition overhead/part | More entered waste and time can outweigh the model's useful material cost. |
Workflow validation checklist
Validate one color-transition plan at a time
Use slicer outputs and explicit business assumptions from the plate being quoted. The checklist does not assign a typical purge amount or AMS performance level.
Inputs to validate
- Compare slices with the same model revision, orientation, quantity, material family, and quality target.
- Enter F and W only when the slicer exposes flush and prime-tower grams; leave unsupported categories unknown.
- Assign the landed price of the material carrying each transition instead of one convenient average.
What to record in your workflow
- Save the slicer version, printer and process profile, plate, color order, and tool-change count.
- Keep single-color and multicolor total time and category grams with the quote revision.
- Record accepted quantity N and the rule used to allocate shared plate overhead across products.
Scenario inputs
- Compare N = 1 with realistic batch quantities to expose how shared overhead changes per part.
- Vary weighted material price and added time ΔT independently before combining their effects.
- Keep missing category values unknown rather than replacing them with a generic purge percentage.
Assumptions & Limitations
Assumptions to replace
- Single-color and multicolor comparisons use the same geometry, quantity, orientation, and quality target.
- Flush and prime-tower grams are entered only when the slicer explicitly reports them.
- Per-color landed prices and the transition sequence come from the intended production job.
- Any example values illustrate the formula and are not a benchmark for AMS waste.
When not to use the result
Where the model can be wrong
- Flush into infill, support, or another object changes the category allocation.
- A shared tower or purge structure is divided by placed rather than accepted parts.
- Orientation changes the number of color-change layers and transition count.
- Color contamination, jams, or rejected surfaces erase the apparent material saving.
1. Separate model, support, flush, and tower material
Use the slicer's material summary to record filament that remains in models, flush or purge material, prime or wipe tower material, and other structures such as brim. Multiply each category by the correct cost per gram. If different spools have different prices, retain the per-material breakdown instead of applying one blended price without documentation.
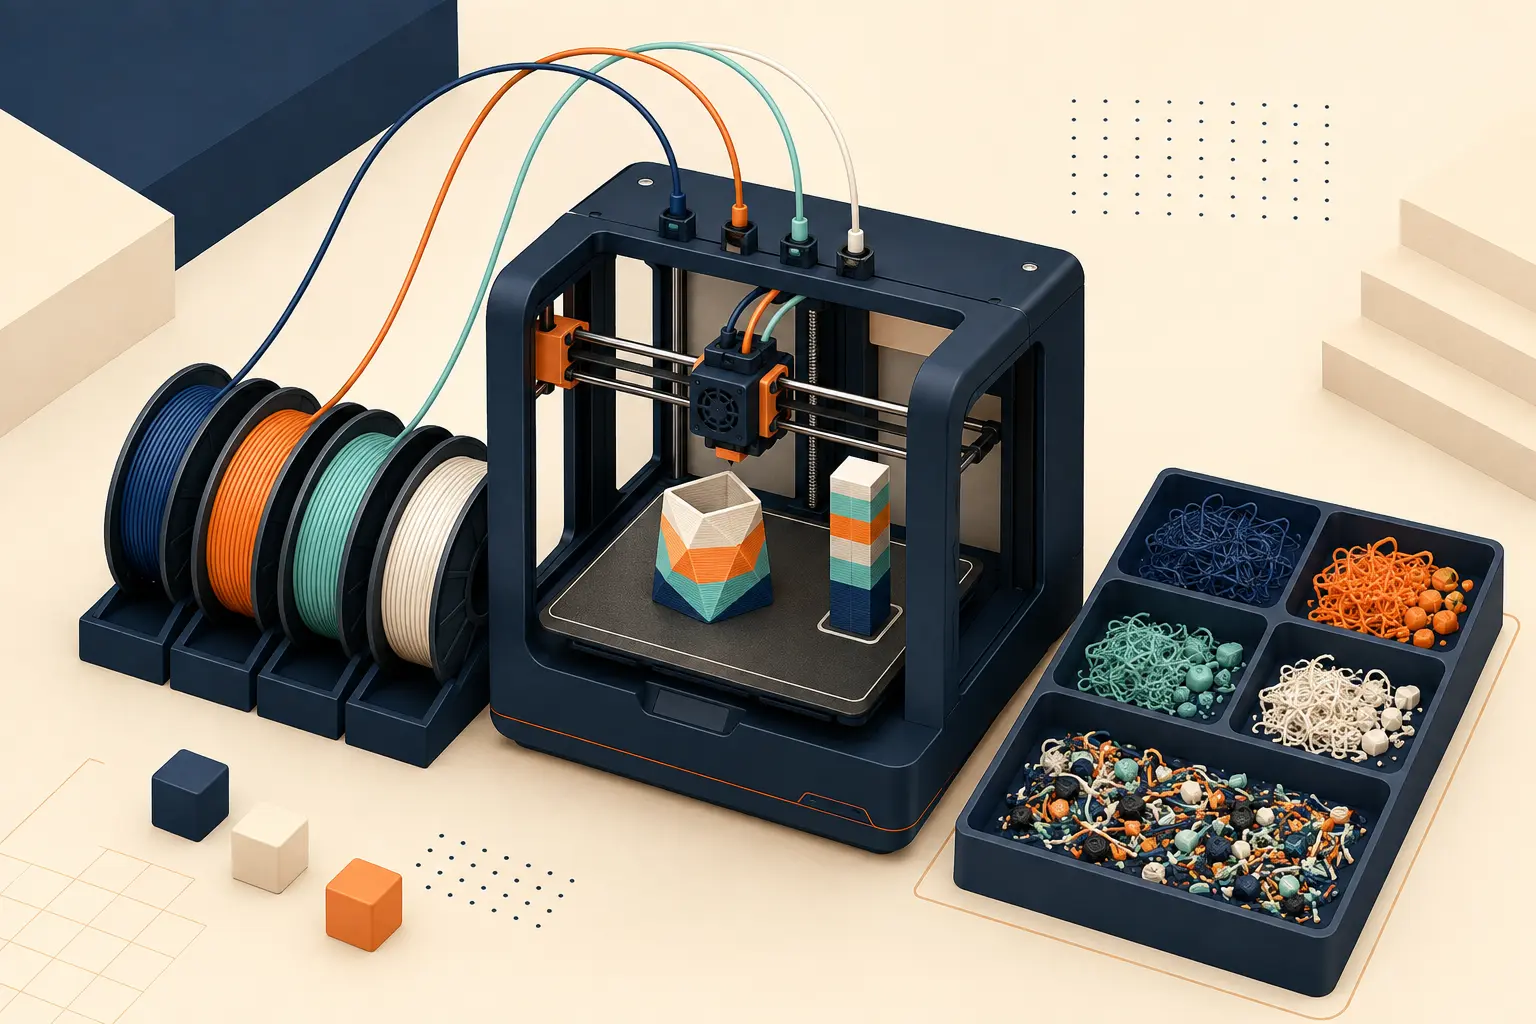
Save the project and summary because a later slicer version or profile may change the calculation. The visible pile beside the printer is only part of the cost; transition routines also add motion and heating time. Compare the multicolor slice with a single-color control to isolate the incremental hours.
2. Count color-change layers, not just the number of colors
A four-color object that changes only twice can be cheaper than a two-color object that alternates on every layer. Inspect the layer timeline and count where tool or material changes occur. Tiny repeated logos, eyes, text, or accents can create a high transition count even though their model volume is small.
When the design allows it, place color boundaries at fewer heights, split decorative pieces for assembly, or orient the model so a color region spans a compact layer range. These are design decisions with appearance and labor tradeoffs, so compare the complete accepted-part cost rather than filament waste alone.
3. Validate transition-specific flush volumes
Dark-to-light transitions often need more cleaning than similar colors or light-to-dark changes. Manufacturer and slicer tools may calculate or suggest volumes, but actual visibility depends on pigment, material, nozzle, temperature, wall thickness, and the product's cosmetic standard. Use a transition sample before reducing production settings.
Change one transition pair at a time and inspect the exterior under consistent lighting. Record the minimum accepted value with the exact spool types. A setting that works for opaque black and red PLA does not prove that translucent or engineering materials will behave the same way.
- Test the most visible dark-to-light transition first.
- Keep material type, nozzle, and temperature with the result.
- Inspect thin light walls for internal color show-through.
- Save only values that meet the product's appearance standard.
4. Use infill or support only when function and appearance allow it
Some slicers can direct transition material into infill, supports, or a separate object. This can reduce discarded material, but internal colors may show through thin or translucent walls. Different materials can also change bonding, mechanical behavior, or support separation. Reuse is not free if it creates rejected parts.
Mark purge objects clearly if their appearance is uncontrolled, and do not sell them as standard-color products without disclosure. Inspect strength-critical areas and top or bottom surfaces after any change. The goal is accepted useful output per purchased gram, not merely a smaller waste-bin number.
5. Spread plate-level transition cost across validated quantities
A wipe tower and many transition events occur at the plate level. Adding several identical models may increase model filament while leaving much of the transition structure shared, reducing purge cost per part. Slice quantities of one, two, four, and a practical full plate to identify where unit cost improves.
Larger batches concentrate failure risk. Validate one or two parts before filling the plate, and divide the final cost by expected accepted quantity. For urgent work, several recoverable plates can be economically safer than one very long plate even when the theoretical unit cost is slightly higher.
6. Price multicolor as a production option, not only extra grams
The incremental cost includes discarded filament, tower material, longer machine occupation, mapping and setup labor, spool handling, monitoring, and a profile-specific failure allowance. Compare the final multicolor job with the equivalent single-color job so the surcharge has a traceable basis.
Customers buy the finished visual result, not purge grams. Use internal cost to establish a safe floor, then price customization, rarity, order quantity, rights, and market value. If batching lowers your cost, you may keep part of the improvement as margin rather than automatically reducing the customer price by the same percentage.
References and further reading
These manufacturer and technical references support the workflow described above. Use them as a starting point, then validate costs and settings in your own workshop.
Test your numbers